

Efficient Air-Powered Conveying Systems for Solving Rice Husk Transportation Challenges
HeadPowder, a leading engineering company based in Shandong, China, specializes in providing advanced solutions for material handling, particularly in the agricultural sector. One of the most challenging tasks in rice processing is the efficient and clean transportation of rice husk, a byproduct that requires specialized equipment to manage effectively.

Understanding the Challenges of Rice Husk Conveying
Rice husk, also known as rice husks or chaff, is a fibrous material produced during the milling process. Its lightweight and dusty nature makes traditional conveyor systems inefficient and prone to clogging or contamination. Conventional methods often struggle with maintaining a consistent flow and preventing dust emissions, which can impact both operational efficiency and worker safety. The need for a reliable, hygienic, and low-maintenance solution has driven the development of air-powered conveying systems tailored for such applications.
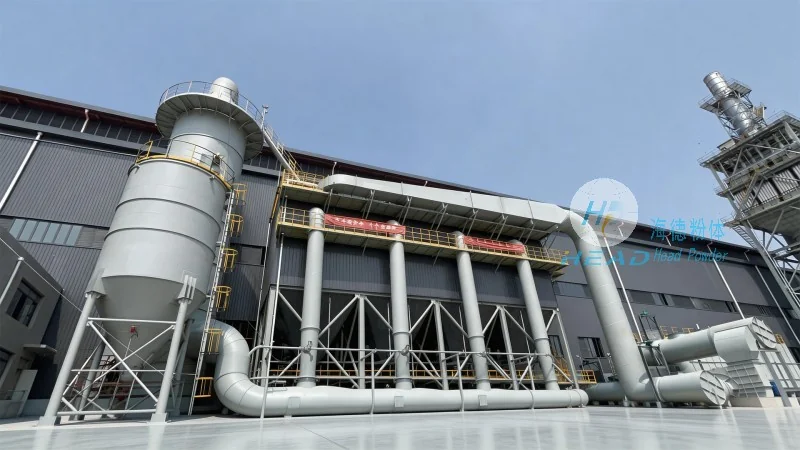
How Air-Powered Conveying Systems Work
HeadPowder's airlock conveying systems utilize a combination of positive and negative pressure to transport rice husk through pipelines. The system operates by creating a vacuum or pressure differential that draws the material into the pipeline using air currents. This method ensures that the material is moved without direct contact, minimizing friction and reducing the risk of contamination. The air-powered design also allows for flexible pipeline routing, enabling the system to navigate complex layouts typical in rice processing facilities.

Key Advantages of Air-Powered Conveying for Rice Husk
Implementing an air-powered conveying system offers several benefits for rice processing operations. Firstly, it provides a dust-free environment, which is crucial for maintaining product quality and meeting hygiene standards. The enclosed system prevents dust from spreading, reducing the risk of respiratory issues for workers and avoiding contamination of other products. Secondly, the system is highly efficient in terms of material handling, with the ability to transport large volumes of rice husk over long distances with minimal energy consumption. This efficiency translates to lower operational costs and increased productivity. Additionally, the air-powered design is low-maintenance, as there are fewer moving parts compared to traditional mechanical conveyors, reducing downtime and repair costs. The system's adaptability also allows for easy integration with existing processing lines, making it a cost-effective upgrade for facilities looking to improve their material handling capabilities.
Customized Solutions from HeadPowder
HeadPowder understands that each rice processing facility has unique requirements. The company offers customized air-powered conveying systems tailored to the specific needs of clients. By working closely with clients, HeadPowder engineers can design systems that optimize material flow, minimize energy usage, and ensure compliance with industry standards. The company's expertise in material handling and its commitment to quality ensure that the systems are built to last and perform reliably under demanding conditions. Whether it's a small-scale operation or a large industrial facility, HeadPowder provides solutions that are both effective and sustainable.

Conclusion
For rice processing plants facing the challenges of rice husk transportation, HeadPowder's air-powered conveying systems offer a reliable and efficient solution. By leveraging advanced engineering and a deep understanding of material handling, the company provides systems that enhance operational efficiency, improve safety, and reduce costs. With a focus on customization and quality, HeadPowder continues to be a trusted partner in the agricultural processing industry, helping facilities overcome the hurdles of material handling and achieve greater productivity.