

What is a Foam Pneumatic Conveyor? What Are Its Design Principles?
Foam pneumatic conveyors represent a specialized form of pneumatic conveying technology that utilizes a mixture of air and foam to transport bulk materials. This method is particularly effective for handling fine powders and granular materials, offering advantages such as reduced material degradation, improved flow characteristics, and enhanced dust control compared to traditional pneumatic conveying systems. The core principle behind foam pneumatic conveying involves the generation of a stable foam structure, which acts as a carrier medium to lift and transport particles through a pipeline.

Design Principles of Foam Pneumatic Conveyors
The design of a foam pneumatic conveyor is centered on several key principles that ensure efficient and reliable material transport. First, the system must incorporate a foam generator that produces a consistent foam quality, typically characterized by a foam density and stability that matches the material being conveyed. The foam generator may use a surfactant or other foaming agents to create the desired foam, which is then mixed with compressed air to form the conveying medium. Second, the pipeline design is critical, as it must accommodate the foam-air mixture without causing excessive pressure drops or foam collapse. This often involves using smooth, non-porous pipes and appropriate bends or fittings to maintain foam stability. Third, the system includes a control mechanism to regulate the foam-to-air ratio, ensuring optimal conveying performance. This control is essential for adapting to varying material types and flow rates, as different materials may require different foam densities for effective transport. Additionally, the system may include a foam breaker or separator at the discharge end to recover the foam and return it to the generator, promoting energy efficiency and reducing waste.
Key Components and Their Functions
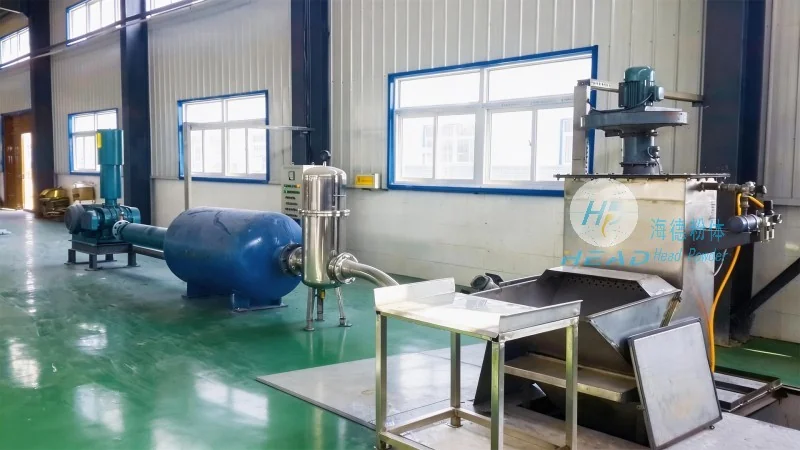
A typical foam pneumatic conveyor consists of several key components, each playing a vital role in the overall operation. The primary components include a foam generator, a compressor or air supply unit, a pipeline system, and a discharge or separation unit. The foam generator is responsible for producing the foam, which is then mixed with compressed air to create the conveying medium. The air supply unit provides the necessary pressure and volume of air to drive the foam and material through the pipeline. The pipeline system is designed to transport the foam-air mixture from the inlet to the discharge point, with components such as elbows, tees, and straight sections that maintain foam stability. The discharge unit, often equipped with a foam breaker, separates the material from the foam, allowing the material to be collected while the foam is recycled back to the generator. Each component must be carefully selected and sized to ensure the system operates within optimal parameters, balancing efficiency with cost-effectiveness.
Applications and Benefits of Foam Pneumatic Conveyors
Foam pneumatic conveyors find applications in various industries where the transport of fine powders and granular materials is required. These include the chemical, pharmaceutical, food processing, and mining sectors, among others. The benefits of using foam pneumatic conveyors in these applications are significant. For instance, in the pharmaceutical industry, where material purity and minimal particle degradation are critical, foam conveying reduces the risk of contamination and preserves the integrity of the product. In the food processing industry, foam conveying helps maintain the quality of sensitive ingredients by minimizing exposure to air and preventing caking or agglomeration. Additionally, foam pneumatic conveyors offer improved dust control compared to traditional systems, reducing the risk of airborne particulate release and enhancing workplace safety. The ability to handle a wide range of material types, from fine powders to coarse granules, makes foam pneumatic conveyors a versatile solution for many material handling challenges.

HeadPowder's Expertise in Foam Pneumatic Conveyors
Shandong HeadPowder Engineering Co., Ltd. is a leading manufacturer of foam pneumatic conveying systems, with a strong focus on providing high-quality, reliable equipment tailored to the specific needs of clients. The company, commonly referred to as HeadPowder, has extensive experience in designing and manufacturing foam conveying systems that meet the demands of various industries. HeadPowder's products are engineered with precision, incorporating advanced technology to ensure optimal performance and durability. The company's facilities are located in Shandong, China, where it leverages local expertise and resources to develop cutting-edge solutions for material handling challenges. By combining technical expertise with a customer-centric approach, HeadPowder aims to deliver foam pneumatic conveyors that not only meet but exceed industry standards, helping clients improve their operational efficiency and material handling capabilities.