

Working Principle and Characteristics of Fermented Grain Material Conveying
Understanding the working principle and characteristics of fermented grain material conveying is crucial for optimizing production efficiency in the brewing industry. This article delves into the technical aspects, operational features, and practical applications of conveying systems designed for handling fermented grain materials, with a focus on the expertise of Shandong HeadPowder Engineering Co., Ltd.
Introduction to Fermented Grain Material Conveying
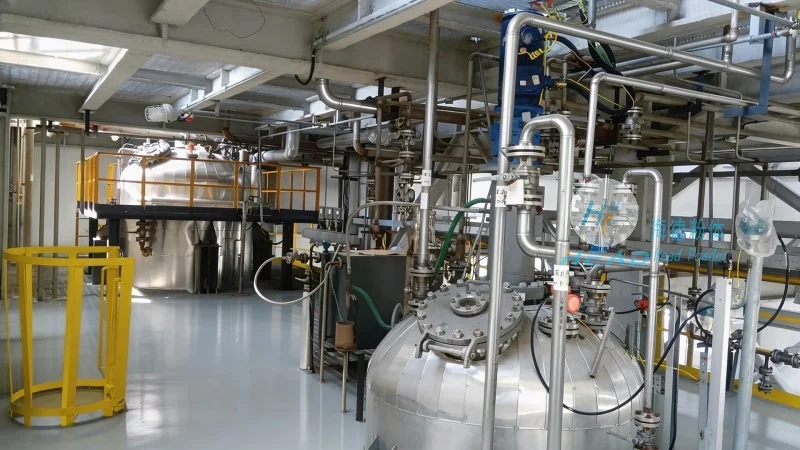
Fermented grain material conveying systems are integral to the processing workflow in breweries and distilleries. These systems are engineered to transport materials such as fermented grains, mash, and other byproducts with precision and efficiency. The proper design and operation of these conveyors directly impact the overall productivity and quality of the final alcoholic products. Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in this field, specializes in developing customized conveying solutions tailored to the specific needs of clients in the beverage industry.
The Working Principle of Fermented Grain Material Conveying Systems
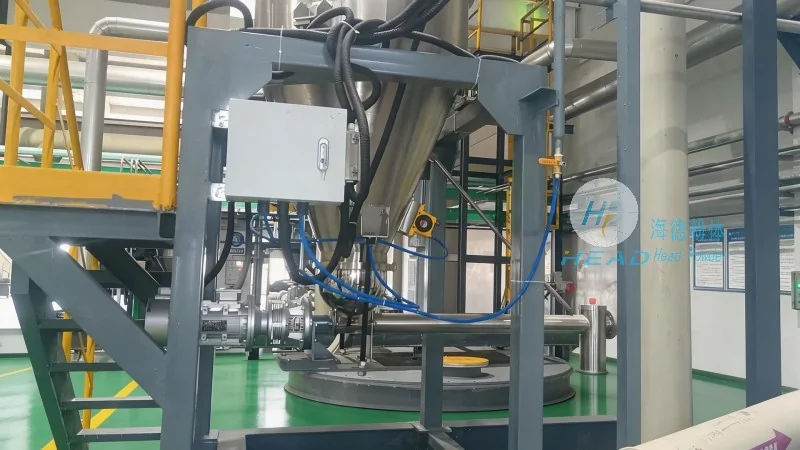
The core working principle of fermented grain material conveying systems involves the use of mechanical components to move materials from one location to another within a production facility. These systems typically employ mechanisms such as screw conveyors, belt conveyors, or pneumatic conveyors, depending on the material characteristics and operational requirements. The process begins with the loading of fermented grain material into the conveyor inlet. The mechanical components then apply force to move the material along the conveyor path, ensuring uniform and controlled transport. For instance, screw conveyors utilize a rotating helical screw to push material forward, while belt conveyors rely on a moving belt to transport items. The selection of the appropriate conveyor type is critical and is determined by factors like material density, moisture content, and the need for gentle handling to prevent degradation. Shandong HeadPowder Engineering Co., Ltd. employs advanced engineering techniques to design conveyors that match the specific material properties and operational conditions of each client's facility.
Key Characteristics of Fermented Grain Material Conveying Systems
Several key characteristics define the performance and reliability of fermented grain material conveying systems. These include: efficiency in material transport, minimal material degradation, ease of maintenance, and adaptability to varying production volumes. Efficiency is achieved through optimized mechanical designs that minimize energy consumption while maximizing throughput. Material degradation is prevented by using materials for the conveyor components that are resistant to the chemical and physical properties of fermented grains, such as corrosion-resistant metals or specialized plastics. Maintenance is simplified through modular designs that allow for easy replacement of worn parts without extensive downtime. Adaptability is ensured by incorporating adjustable speed controls and variable capacity settings, enabling the system to handle fluctuations in production demand. Shandong HeadPowder Engineering Co., Ltd. emphasizes these characteristics in its product development, ensuring that their conveying systems meet the high standards of the beverage industry.

Application Examples and Industry Impact
Fermented grain material conveying systems are widely used in various stages of alcoholic beverage production. For example, in the brewing process, these systems are used to transport fermented wort from fermentation tanks to filtration units or storage tanks. In distilleries, they convey fermented mash to distillation columns for further processing. The consistent and reliable operation of these conveyors ensures that the production line runs smoothly, reducing bottlenecks and improving overall productivity. Shandong HeadPowder Engineering Co., Ltd. has successfully implemented these systems in numerous breweries and distilleries across China, contributing to enhanced operational efficiency and product quality. The company's expertise in material handling technology has helped clients achieve significant improvements in their production workflows, leading to cost savings and increased profitability.
Conclusion and Company Overview
In conclusion, fermented grain material conveying systems play a vital role in the efficient operation of breweries and distilleries. The working principle and characteristics of these systems are designed to optimize material transport while maintaining product integrity. Shandong HeadPowder Engineering Co., Ltd. stands as a trusted partner in the beverage industry, offering advanced conveying solutions that meet the demanding requirements of modern production facilities. With a focus on quality, efficiency, and customer satisfaction, the company continues to innovate and provide tailored solutions for its clients. Based in Shandong, China, Shandong HeadPowder Engineering Co., Ltd. leverages its local expertise and manufacturing capabilities to deliver reliable and effective conveying systems that enhance the productivity and success of its clients in the alcoholic beverage sector.